This article offers a comprehensive guide to Production Planning as a strategic lever for the Supply Chain. It starts with the definition of excellent Supply Chain and the central role of Planning, then explores production strategies (ETO, MTO, ATO, MTS) and the impact of production layout. The hierarchy of planning—from S&OP to Master Scheduling, from MRP to Capacity Planning—is illustrated, with insights into Demand Planning, material policies, and capacity sizing. The journey concludes with the concrete results achievable from an integrated system and guidance on how to initiate change in your own organization.
In an industrial landscape characterized by volatility, increasingly shorter life cycles and increasing pressure on costs, production planning is no longer a simple operational process. It has become a strategic lever. Its ability to orchestrate demand, resources, materials and production capacity in an integrated manner allows companies to ensure continuity, service levels, margins and sustainable growth.
An effective production planning model is not limited to determining what to produce and when: it creates a common language within the company, aligns functions, defines rules, processes, and tools that make the decision-making flow clear, stable, and measurable.
This article offers a comprehensive and structured reading of the main pillars of the model: from the definition of the Supply Chain to production strategies, from Demand Planning to Sales & Operations Planning (S&OP), to Master Scheduling, MRP and Capacity Planning logic. A journey that shows how only a true integrated planning system can transform complexity into competitive advantage.
The Supply Chain is the global network of structures, information and physical flows that enables the transformation of raw materials into a finished product and its delivery to the final customer. Supply Chain Management encompasses the design, planning, execution and control of all these activities with the goal of creating value, synchronizing demand and supply, reducing variability and ensuring end-to-end performance.
Planning sits at the heart of this ecosystem, because it represents the connection between corporate strategy and operationality. It is here that objectives, budgets, and business priorities are translated into concrete plans for production, procurement, and distribution.
The first variable to understand when building an effective planning system is the production strategy adopted by the company. The four main strategies – Engineer to Order (ETO), Make to Order (MTO), Assembly to Order (ATO), and Make to Stock (MTS) – profoundly influence downstream processes: from forecasting, to inventory management, to Master Scheduling and MRP.
The choice depends on factors such as:
In the typical life cycle of a product, ETO and MTO predominate in the launch and growth phases, while ATO and MTS are more common in maturity, when volumes increase and standardization becomes a priority objective.
Defining one’s strategy (or strategies, if there are different mixes) correctly is essential: each model involves a different point of decoupling between forecasts and client orders, and therefore requires a different organizational structure and a different planning approach.
The production layout also significantly influences the planning model.
The main types are:
Each layout requires a specific planning model. For example, in a continuous or process context, it will be natural to adopt capacity planning as the primary driver, while in MTO on-demand contexts, orders and materials will be the priority.
Effective planning is not a single process, but a hierarchical system that connects different time horizons and different levels of granularity:
The quality of execution depends on the alignment of all these levels. A weak S&OP, for example, generates downstream instability in MPS, MRP, and scheduling, with heavy impacts on inventory and service level.
Demand planning combines statistical and qualitative techniques to build the expected demand for products or services. The demand can come from:
Typical patterns (trend, seasonality, random variability) influence the choice of forecasting techniques and the stockkeeping policies.
The fundamental principles are clear:
The main indicators include:
MAD: Mean Absolute Deviation
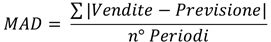
This indicator aims to determine the deviations between demand and forecasts, plan around the error, and properly dimension the safety stock, thereby improving forecasting techniques.
BIAS: the tendency to deviate from the average value
MAPE (absolute average error percentage)
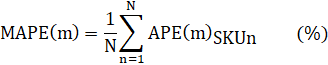
measured through monitoring dashboards.
With
The XYZ Classification of the historical demand for products (variability) is used to assign each item the demand variability class. It is based on calculating the Coefficient of Variability and the demand density.

σ sigma : is the standard deviation of the historical series of demand
µ media: is the average of the demand
ABC indicator: is a classification of materials that can be used to filter them in planning transactions to allow for a more intelligent management of the product portfolio and stock policies.
Sales & Operations Planning is the process that integrates all corporate plans – sales, marketing, product development, production, procurement, and finance – into a single monthly tactical plan. It is the point of contact between strategy and operations.
The S&OP process consists of five steps:
The benefits are manifold:
Without a stable and disciplined S&OP, every subsequent phase of planning becomes reactive, fragmented, and inefficient.
Resource Planning (RP) aims to verify the feasibility of the plan defined by S&OP in the medium-long term. It uses the Bill of Resources, a simplified breakdown that represents the average supply required for a product family.
The process allows for:
The Master Production Schedule (MPS) translates the S&OP plan into a production schedule for individual codes, with precise quantities and dates.
The objectives of the MPS are:
The disaggregation of the plan is fundamental and is based on coefficients derived from historical analysis. The structure of the planning changes depending on the strategy:
ATP is defined as the stock and planned orders that have not yet been used to fulfill customer orders. It does not consider commitments derived from forecasts but only from confirmed customer orders. It is of 2 types:
To properly manage customer promises, which is an essential element for reliability and service level.
The definition of the planning time fences is crucial; they stabilize the plan and prevent continuous changes, which are one of the main causes of inefficiency and hidden costs.
It is the engine that, starting from the MPS and the Bill of Material (BOM), calculates the net requirements, proposing production and purchasing orders.
To function properly, it requires impeccable demographic data:
The calculation logic is based on Low Level Code (LLC), which defines the order in which the BOM is exploded. Exceptions (anticipations, postponements, cancellations) must always be monitored through pegging functionality, which allows tracing back to the source of the requirements.
In the event of an exception or a change in the arrival schedule of materials, it is important to trace the source of the needs to understand the impacts on higher levels.
An MRP that works with unreliable data generates overstocking, stock-outs, emergencies, plan instability, and an overall increase in costs.
The choice of procurement policy has crucial impacts on inventory levels, costs, and service levels.
Among the main methods:
Each technique has a specific logic and a recommended application based on variability, order code value, order issuance costs, and demand dynamics.
Even advanced practices such as VMI (Vendor Managed Inventory) and Consignment Stock can improve efficiency and reduce operational burden, especially for Class C or D materials.
Capacity planning allows to verify whether the material plan is consistent with the production resources.
Capacity Requirement Planning (CRP) is based on:
The difference between:
determines different approaches and different leveling strategies.
The CRP is essential to avoid unmanaged workloads and to ensure reliability in delivery. Analyses such as queueing, waiting times, and the application of the Little law (the average number of customers in a system is equal to the average arrival rate multiplied by the average time in the system) allow us to understand how saturation affects the overall lead time.
Industrial competition is no longer just about the product, quality or price; it is about the ability to reliably plan demand, capacity and materials throughout the entire supply chain.
Based on our experience, an integrated Production Planning model can bring the following benefits:
Stock reduction: up to – 30 – 40%
Improved indices: OTD (On-Time Delivery) and OTIF (On-Time In-Full)
Reduction of Lead Time
Guarantee of the stability of the plan
Increase in production efficiency.
For many companies, the first step is not to implement a new tool, but to rethink the architecture of the planning processes – from Demand Planning to S&OP, from MPS to Capacity Planning – in an end‑to‑end and data‑driven way.
If you want to understand where to start in your own reality, discover our approach to Lean Production Planning & Demand Planning and how we integrate digital processes and tools into planning. To learn more in a practical way, you can consider the course "Effective Production Planning" from the Lean Factory School®, which brings real-world cases and operational tools directly applicable to your company into the classroom. A robust, integrated, and data-driven planning system will be the ones able to overcome the challenges of the future.
Incorrect data (lead time, minimum quantities), inaccurate BOM or lack of Planning Time Fence cause continuous exceptions. Result: stock-outs, extra costs and instability. Solution: validate the basic parameters, use pegging to track the impacts and monitor the MRP dashboard.
Forming a cross-functional team (sales, operations, finance), collecting key data (sales, inventory, capacity), and launching a monthly cycle: Data Gathering, Demand Review, Supply Planning, Pre-S&OP, Executive Meeting. Measuring with KPIs such as forecast accuracy (>80%) and inventory turns.
It depends on variability and item value: EOQ for high fixed costs, Lot-for-Lot for stable demand, min-max for C/D items. Use ABC-XYZ to prioritize and consider VMI for reliable suppliers. Goal: balance holding costs vs. ordering.
Available To Promise (ATP): stock + planned orders not allocated to confirmed customers (excludes forecasts). It manages realistic promises by calculating discrete or cumulative availability. It sets Time Fence to stabilize and improve OTD/OTIF.
KPI tracking: OTD/OTIF (>95%), inventory reduction (20-40%), forecast accuracy (MAPE <20%), emergencies (<10%), OEE productivity. Benchmark: integrated systems reduce inventories by 30% and stabilize plans within 6-9 months
Did it help you? Add it as your preferred source on Google


 ai translated